SMART FACTORY SOLUTIONS
Smart Factory solutions for a connected, intelligent operation.
Your machines, systems and people already generate the data you need to run a better operation. CAD-IT connects MES, Industrial IoT and your existing OT/IT systems into one Manufacturing Intelligence Hub, turning that data into real-time insight on the factory floor and in the field.
Siemens Silver Expert Software PartnerFactorise MES partnerISO 9001 & ISO 14001
The Smart Factory Explained
What is a Smart Factory?
A Smart Factory is a manufacturing operation in which equipment, systems and people are digitally connected, so production data is captured automatically, put into context and used to make faster, better decisions.
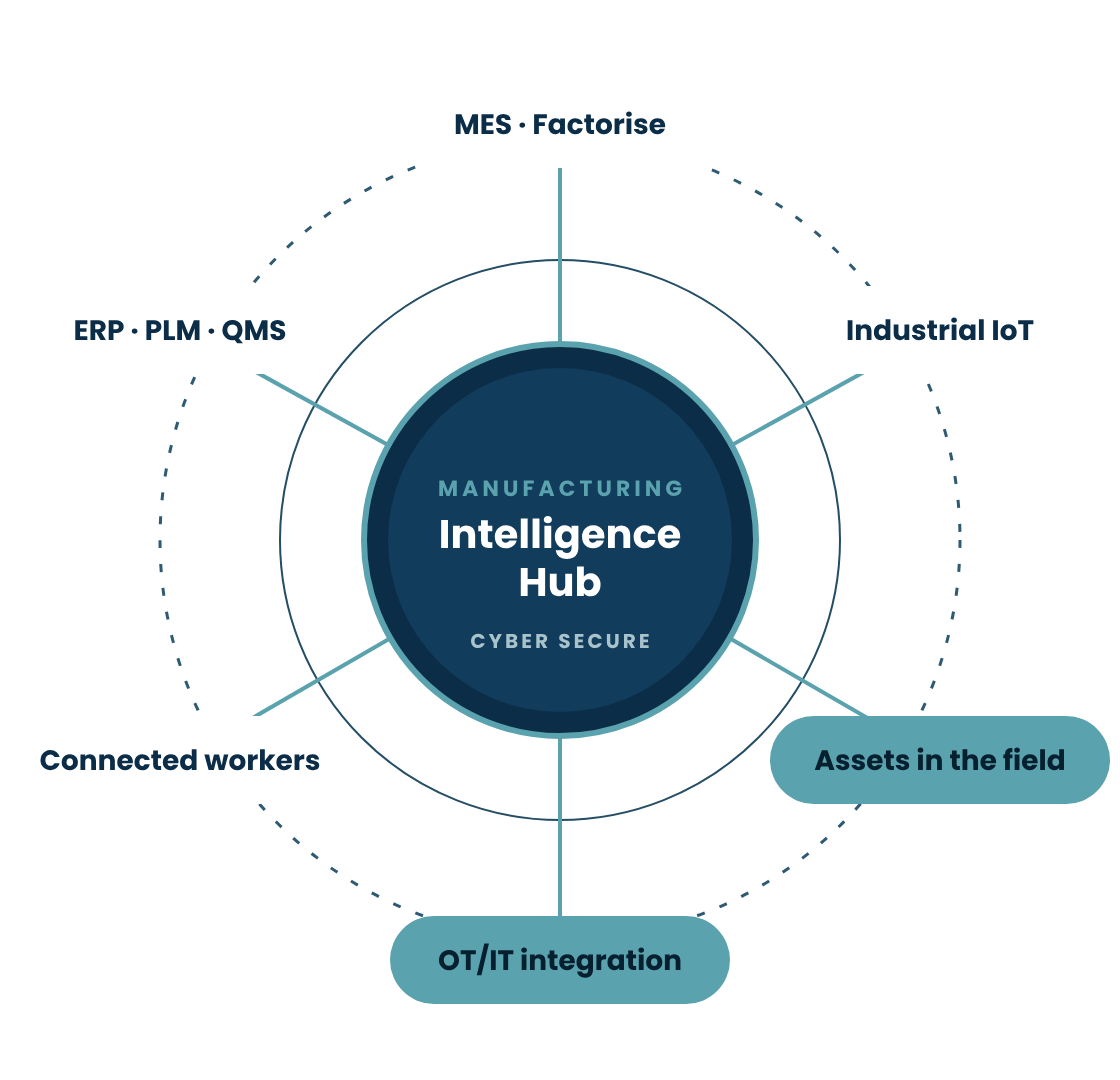
It isn't a single product. It's a joined-up approach: a Manufacturing Execution System (MES) runs and records production, Industrial IoT (IIoT) connects machines and assets, and an intelligence hub brings it all together with your ERP, PLM and quality systems. The result is one version of the truth, from the shop floor to the boardroom and out to equipment in the field.
Sound familiar?
A connected operation fixes the root cause: disconnected data.
How it all comes together
From the factory floor to real-world results.
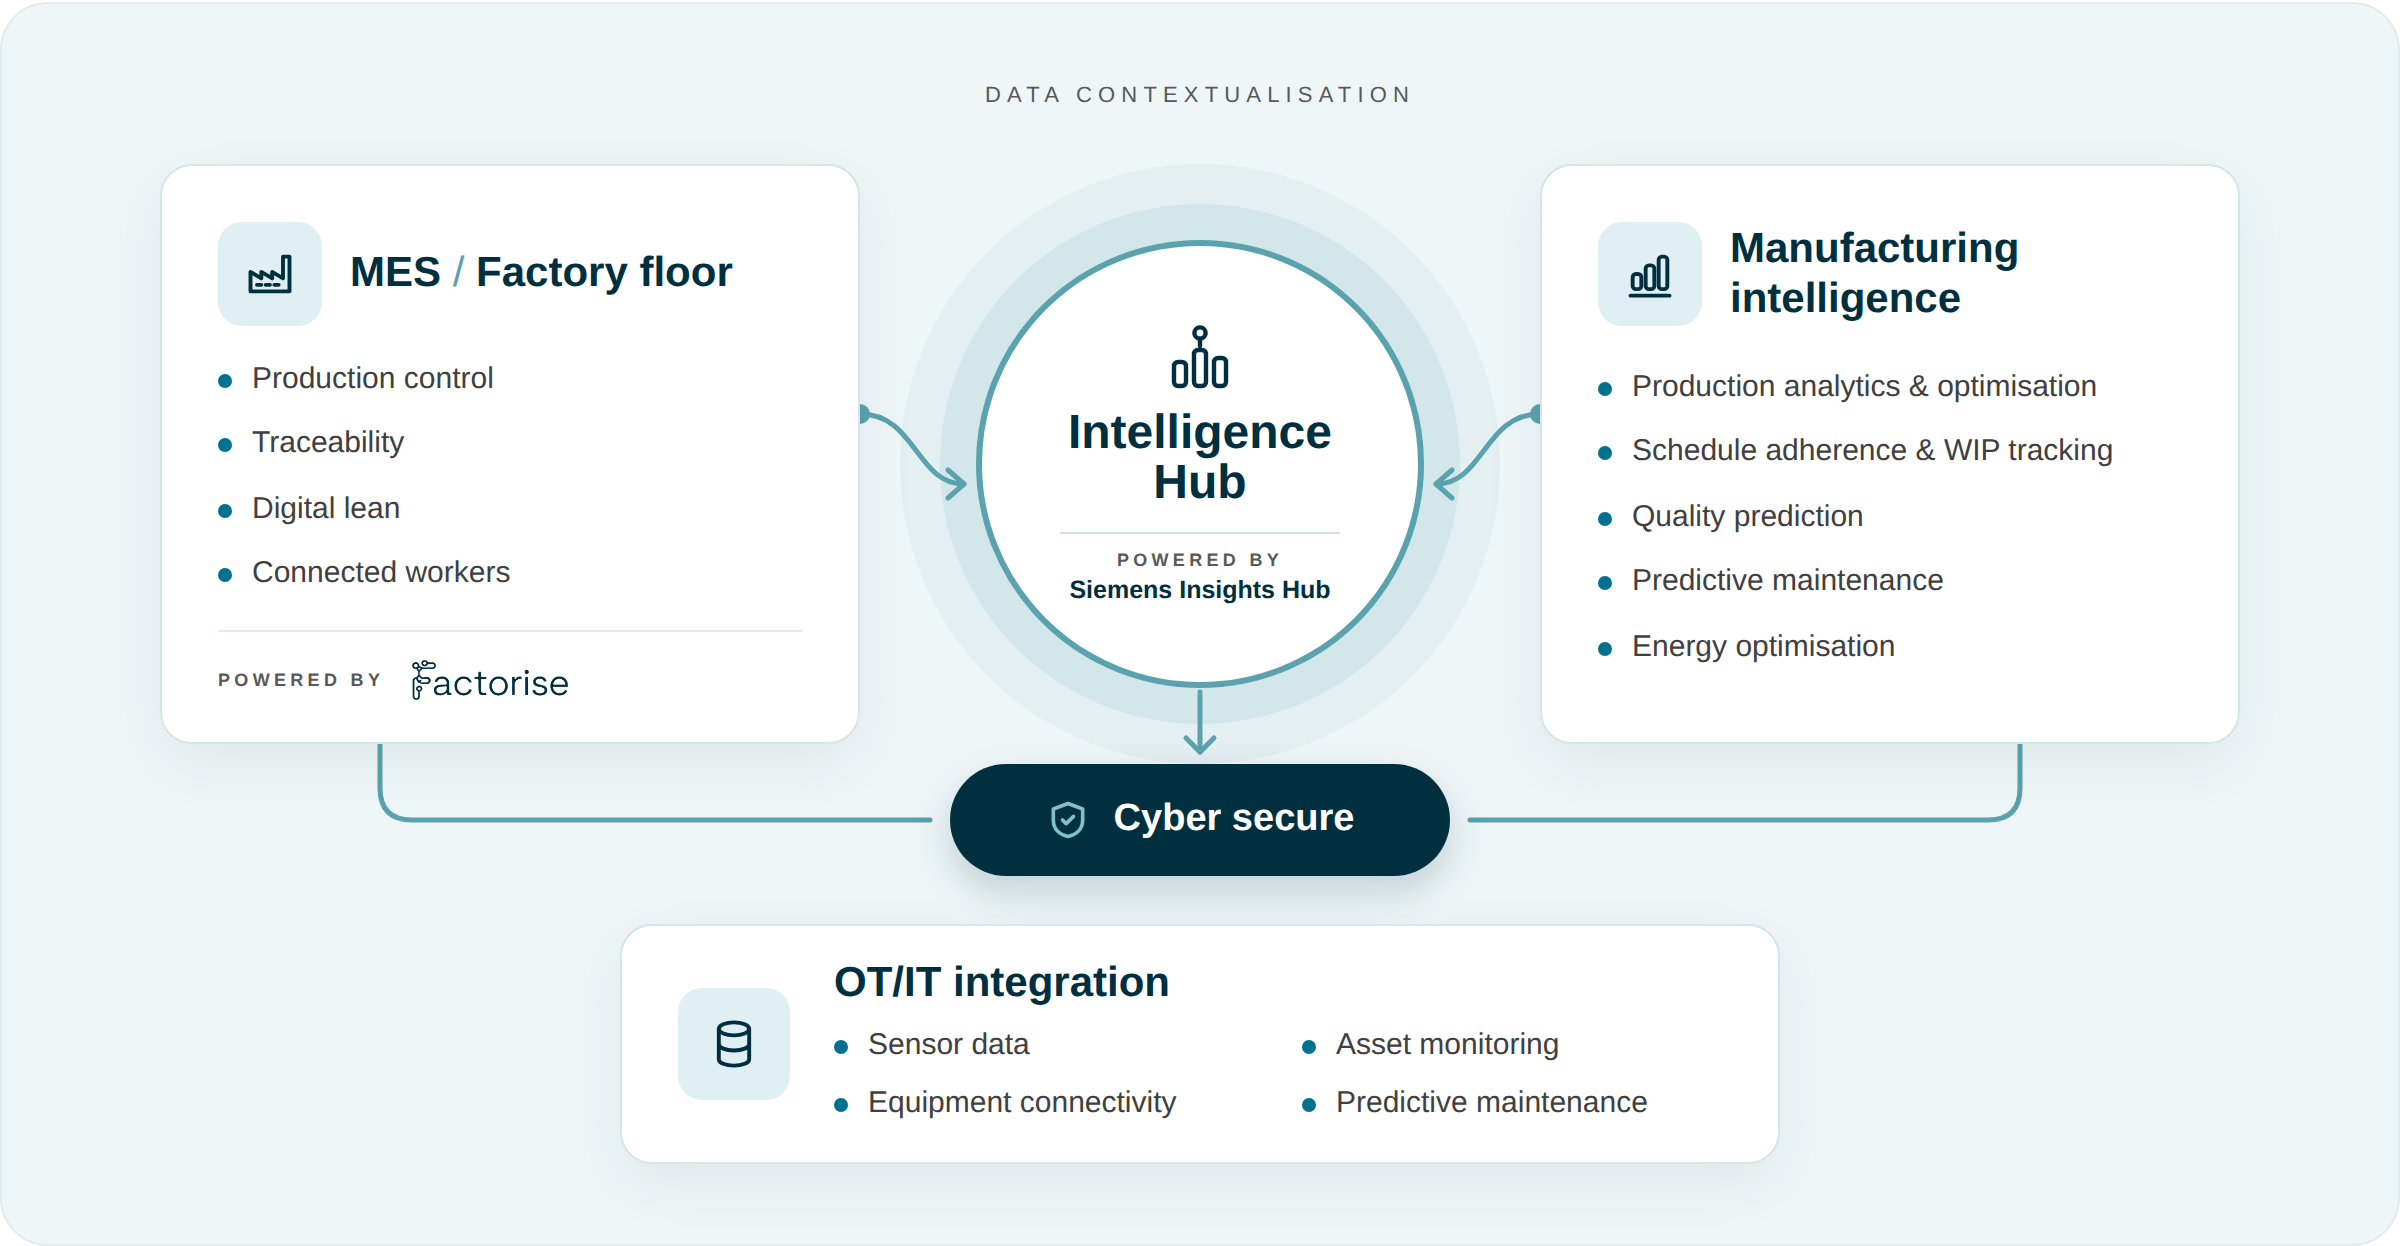
At the centre sits the Intelligence Hub. It contextualises data from your machines and MES, then feeds manufacturing intelligence back to the people who need it — securely, end to end.
01 · Connect
Link every asset
Link machines, sensors and legacy equipment, new or old, so data flows automatically.
02 · Integrate
Bring OT and IT together
Connect MES and IoT with ERP, PLM and quality systems.
03 · Digitalise
Go paperless on the floor
Replace paper and spreadsheets with digital workflows, traceability and live dashboards.
04 · Deliver
Turn data into results
Turn connected data into measurable results, and keep improving with continued support.
Our Smart Factory solutions
Better together.
Start where the value is greatest for you: running and recording production with MES, or connecting your assets with Industrial IoT. Both feed the same Intelligence Hub, so you can add the other when you're ready.
MES · Factorise
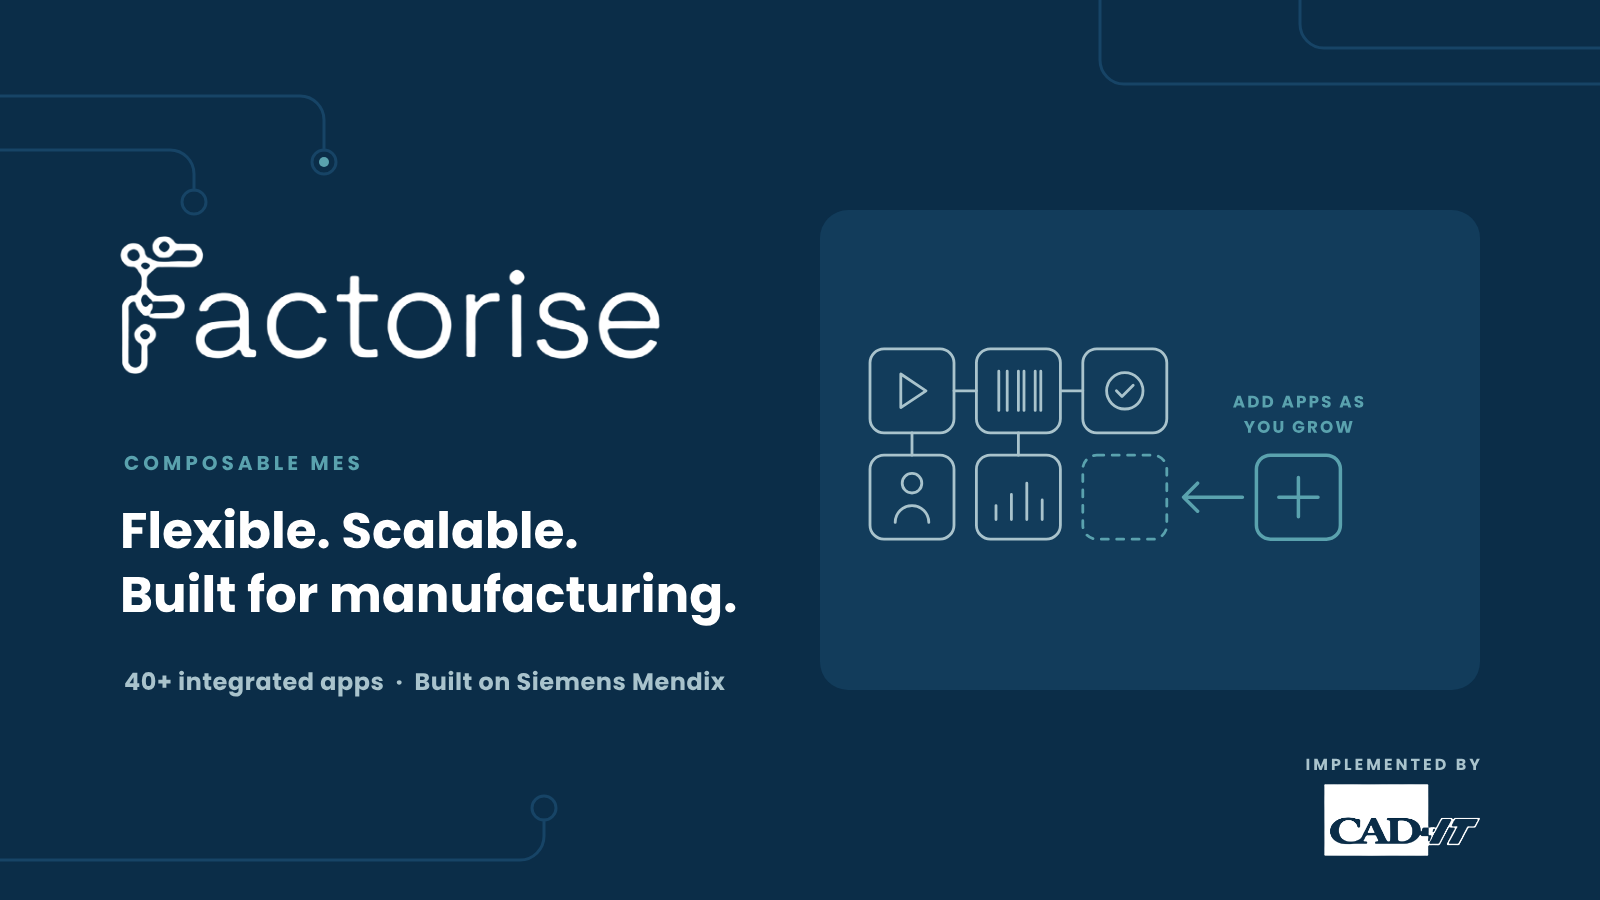
Factorise MES: composable MES that grows with you
A cost-effective, scalable and flexible Manufacturing Execution System, built for SMEs. Start with the apps you need today and add more as you grow, with CAD-IT connecting it seamlessly to your OT/IT systems.
Industrial IoT · Siemens
Siemens Insights Hub: Industrial IoT that turns asset data into action
Siemens Insights Hub is a comprehensive Industrial IoT platform that connects your physical assets to your digital systems. CAD-IT helps you connect equipment, surface the insights that matter and scale from one line to every site.
KEY OUTCOMES AND BENEFITS
The benefits of a smarter, connected operation.
Optimised production efficiency
Maximise throughput, reduce cycle times and make the most of every resource.
Reduced operational costs
Lower maintenance spend with predictive insight, less downtime and less waste.
Enhanced product
quality
Tighter quality control, fewer defects and rework, and faster root cause analysis.
Real time visibility and decision making
Instant access to live KPIs, so decisions are based on data, not guesswork.
Improved agility & responsiveness
Adapt quickly to change and respond faster to customer demand.
An empowered workforce
Critical information at people's fingertips, streamlined workflows and continuous improvement.
Improved sustainability
Optimise energy use and reduce waste, supporting your environmental targets.
Where could you gain the most?
We'll help you find the quickest wins in your operation.
Beyond the factory floor
Connected operations, in the factory and in the field.
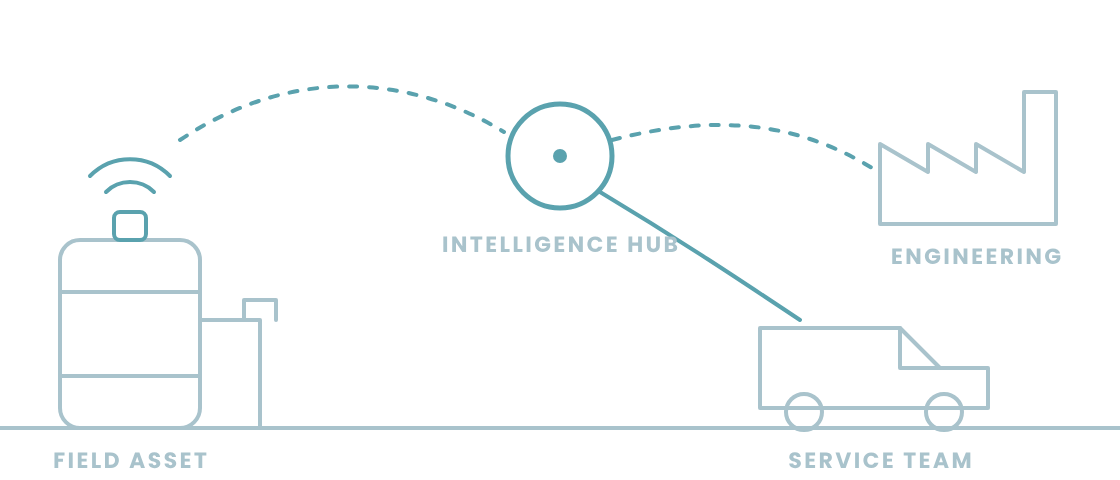
A smart operation doesn't stop at the factory gate. The same connected approach extends to the equipment you've sold and installed at customer sites. Condition and performance data flows back to the Intelligence Hub, so service teams can act before a failure and engineers can learn from real-world use.
Remote asset monitoring
See the health and performance of equipment in the field without sending an engineer.
Predictive, planned service
Move from reactive call-outs to planned interventions that protect your customers' uptime.
Closed-loop engineering
Feed real-world performance data back into design and manufacturing to build better products.
Why CAD-IT?
Clear roles, greater outcomes.
Technology is only valuable when it solves a real problem. We pair leading Siemens-based platforms with the implementation expertise to make them work in your operation, not just on paper.
Implementation expertise
From scoping and configuration to go-live and beyond, our team turns technology into real-world results, with success plans that keep value growing.
Integration with your ecosystem
We connect new solutions with what you already run, from shop-floor equipment to ERP and PLM, so nothing works in isolation.
Sector knowledge
We understand manufacturing and service operations, and we speak the language of both your production and IT teams.
Case study · CDE Group
From a two-asset pilot to more than 80 connected plants in 18 months.
CDE connected its global wet-processing plants with Siemens Insights Hub, giving teams real-time visibility of energy, water and chemical use.
80+
connected plants worldwide
18 months
from pilot to global network
Ready to build your Smart Factory?
Every organisation has a unique set of requirements. Tell us where you are today and we'll help you map the quickest route to a connected, data-driven operation, whether you're starting with one line or scaling across sites.
Technology and accreditation partners